
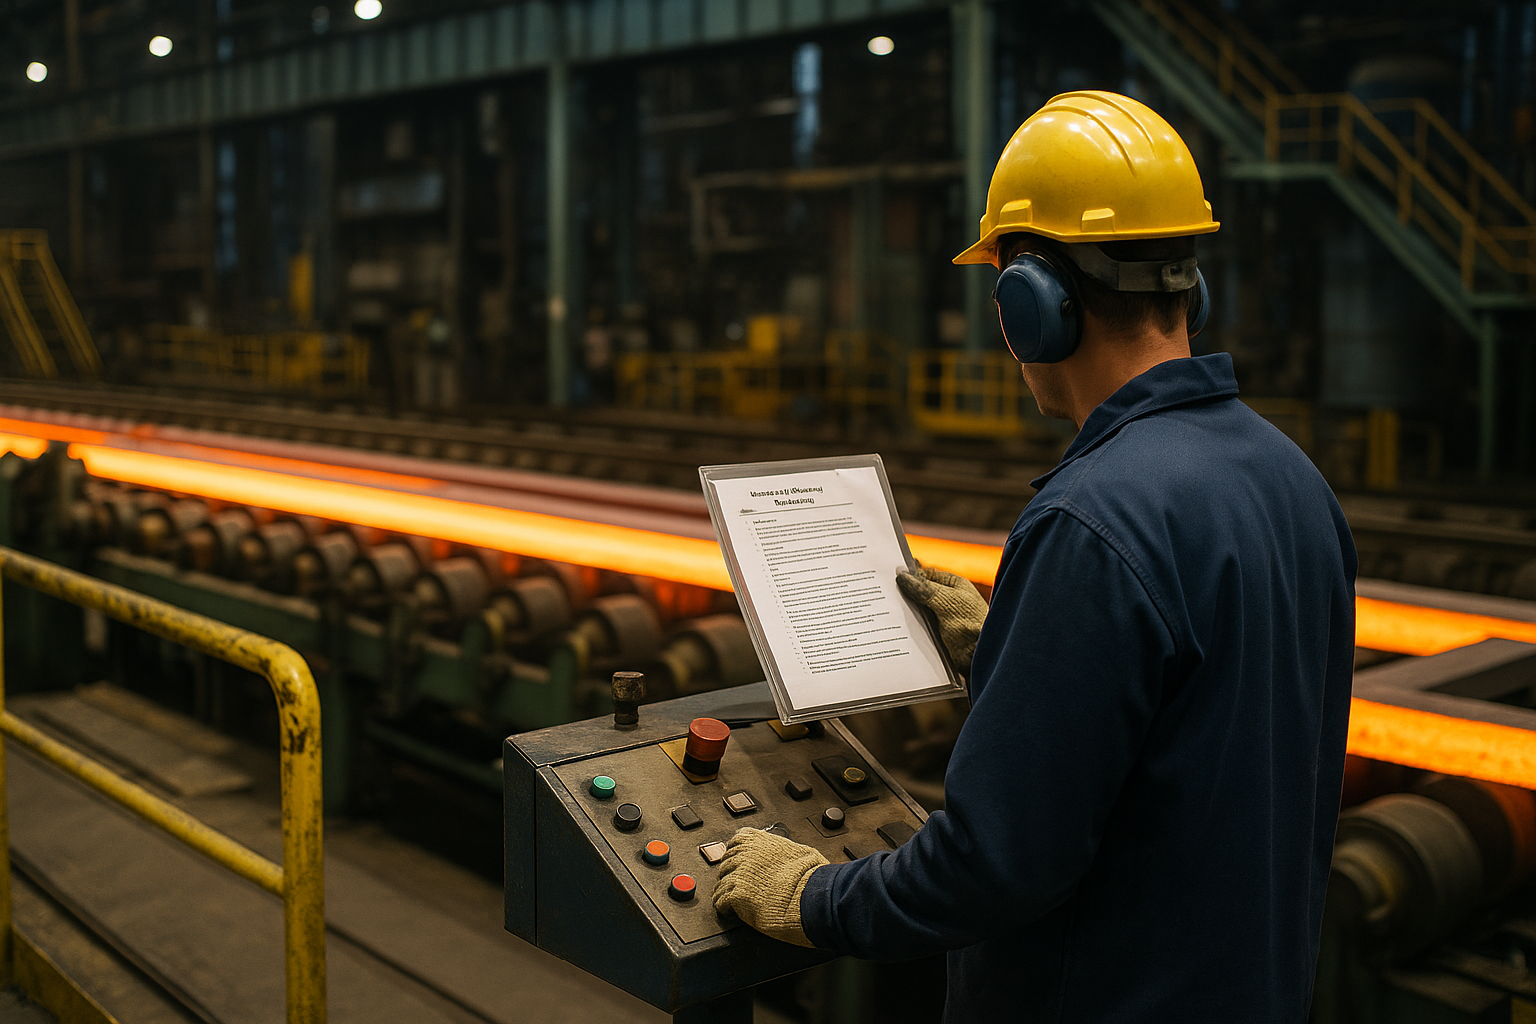
Steel plants operate in an environment where small deviations can create disproportionately large consequences.
A change in furnace practice, an incorrect inspection sequence, a missed lubrication point, an inconsistent sampling method or an improperly executed coil-handling procedure can affect productivity, quality, safety, energy consumption and ultimately cost.
This is why operational excellence in steel manufacturing depends not only on advanced equipment and experienced professionals, but also on the ability to convert technical knowledge into repeatable operating practices.
Standard Operating Procedures (SOPs) are one of the fundamental tools for achieving this objective.
However, an SOP should not be understood simply as a document describing how an activity is performed.
A well-designed SOP is part of a broader process-control system connecting:
process knowledge + operating parameters + responsibilities + safety + quality criteria + records + deviation management + continuous improvement.
When these elements work together, SOPs can help steel plants reduce process variability, preserve technical knowledge and improve operational discipline across shifts, teams and production areas.
What Is a Standard Operating Procedure?
A Standard Operating Procedure is documented information describing the standardized method established by an organization for performing an activity or process.
In industrial environments, SOPs commonly define elements such as:
- purpose and scope;
- responsibilities;
- prerequisites;
- equipment and materials;
- operating sequence;
- process parameters;
- safety requirements;
- inspection points;
- acceptance criteria;
- required records;
- actions for abnormal conditions;
- references to related documents.
This distinction is important because an SOP is not simply a checklist.
A checklist verifies that specific actions or conditions have been addressed. An SOP explains the controlled method by which an activity should be executed.
Likewise, an SOP should not necessarily contain every detailed movement required for every task.
That is where the distinction between procedures and work instructions becomes useful.
SOP vs. Work Instruction vs. Checklist
These documents perform related but different functions.
A procedure generally establishes what must be done, by whom, under which conditions and according to which controls.
A work instruction normally provides more detailed guidance on how a specific task should be performed.
A checklist helps verify that required steps, conditions or inspections have been completed.
A record provides evidence of what actually occurred.
For example, a steel plant may have an SOP governing coil inspection. That SOP could reference:
- a work instruction explaining how to measure thickness;
- a visual defect classification standard;
- an inspection checklist;
- a form recording measurements and disposition.
The distinction is consistent with quality-management principles in which documented information supports the operation and control of processes rather than becoming an objective in itself.
This leads to an important principle:
The objective is not to create more documents. The objective is to create more controlled processes.
Why SOPs Matter in Steel Production
Steelmaking combines complex equipment, high temperatures, material transformation, chemical reactions, mechanical processing and strict product requirements.
At the same time, many plants operate continuously with different crews working on the same equipment.
Without effective standardization, operational knowledge can gradually become dependent on individual experience.
One shift performs an operation one way.
Another shift makes a small adjustment.
An experienced operator develops an informal shortcut.
A new employee learns the process differently.
Over time, these differences can become process variation.
Effective SOPs establish a common operational baseline.
1. SOPs Reduce Process Variability
Variation is one of the central challenges of industrial process control.
Not all variation is harmful. Raw materials, equipment conditions and product requirements naturally change.
The problem arises when unnecessary variation is introduced by inconsistent operating practices.
Consider operations such as:
- furnace charging;
- alloy additions;
- ladle preparation;
- casting start-up;
- roll change;
- line threading;
- surface inspection;
- coil sampling;
- equipment lubrication;
- product packaging.
If different operators execute these activities using significantly different methods, the process itself gains another source of variability.
SOPs help define the approved operating method.
That does not eliminate professional judgment. Instead, it establishes the standard condition from which deviations can be identified and evaluated.
2. SOPs Help Stabilize Quality Across Shifts
Steel customers purchase products according to specifications.
Depending on the product, requirements may involve:
- chemical composition;
- dimensional tolerances;
- mechanical properties;
- flatness;
- surface quality;
- coating mass;
- hardness;
- microstructure;
- weldability;
- formability.
Meeting these requirements consistently requires more than final inspection.
Quality must be controlled throughout the process.
SOPs can connect operating activities with critical quality characteristics by defining inspection points, measurement methods, acceptance criteria and escalation rules.
This is especially important when the same process is operated by multiple crews.
The customer should not receive a different product because the coil was manufactured during a different shift.
3. SOPs Preserve Industrial Knowledge
Experienced operators, technicians and engineers accumulate enormous amounts of practical knowledge.
They learn:
- which signals indicate process instability;
- which equipment behaviors require attention;
- which defects tend to follow certain operating conditions;
- which parameters interact;
- which abnormalities should trigger escalation.
If this knowledge exists only in people’s experience, the company carries a significant organizational risk.
Retirement, turnover, internal transfers or expansion can remove critical knowledge from the operation.
Good procedures and work instructions help transform individual knowledge into organizational knowledge.
This does not mean documenting every piece of tacit experience.
It means identifying knowledge critical to process reliability and incorporating it into controlled operating practices.
4. SOPs Improve Training and Qualification
Training a new steel-plant employee exclusively through observation can create inconsistencies.
The employee may learn what an experienced operator normally does without understanding:
- why the step is required;
- which parameter is critical;
- what constitutes an abnormal condition;
- when the process must be stopped;
- when supervision or engineering must be contacted.
A structured training system can use SOPs as one component of qualification.
For critical activities, qualification may combine:
theoretical training → procedure review → supervised practice → competency verification → authorization.
This is substantially stronger than assuming that reading a procedure automatically makes someone competent.
An SOP is a training resource.
It is not a substitute for training.
5. SOPs Support Safer Operations
Steel plants contain substantial hazards, including:
- molten metal;
- high-temperature surfaces;
- moving machinery;
- overhead loads;
- pressurized systems;
- gases;
- electrical equipment;
- chemicals;
- confined spaces.
Procedures can integrate mandatory safety controls directly into the operating sequence.
Depending on the task, these controls may include equipment isolation, permits, PPE, lockout/tagout requirements, gas testing or communication protocols.
The important concept is integration.
Safety should not appear as an unrelated paragraph at the end of an operating document. Critical controls should be incorporated into the activity where they are required.
At the same time, an SOP must never be treated as a substitute for formal hazard analysis, engineering safeguards or regulatory requirements.
6. SOPs Improve Maintenance Discipline
Maintenance performance is strongly affected by consistency.
Routine tasks such as:
- lubrication;
- inspection;
- alignment verification;
- filter replacement;
- vibration measurement;
- hydraulic inspection;
- sensor checking;
- torque verification
can appear simple.
Yet inconsistent execution may eventually contribute to equipment degradation or unexpected failures.
Maintenance procedures can define not only the task but also:
- inspection frequency;
- measurement method;
- acceptable range;
- required tools;
- lubrication specification;
- recording requirements;
- escalation criteria.
This becomes especially powerful when SOPs are integrated with a Computerized Maintenance Management System (CMMS).
The procedure explains the standard method.
The CMMS manages when the activity is required.
The record demonstrates what was performed.
The condition data supports future maintenance decisions.
7. SOPs Strengthen Root Cause Analysis and CAPA
When a quality problem or operational failure occurs, one of the first questions should be:
Was there a defined standard?
Then:
Was the standard followed?
These questions separate different types of problems.
If no adequate standard exists, the system itself may be deficient.
If the standard exists but was not followed, training, accessibility, supervision or usability may be involved.
If the standard was followed and the failure still occurred, the procedure or process design may require improvement.
This distinction makes root cause analysis more rigorous.
Corrective and Preventive Action (CAPA) should therefore not automatically conclude with “revise the SOP.”
Sometimes the real corrective action is equipment modification, process redesign, better measurement, improved training or stronger engineering controls.
8. SOPs Support the Process Approach of ISO 9001
ISO 9001 emphasizes a process approach, documented information, monitoring, measurement and continual improvement. It does not prescribe that every organizational activity must have a lengthy written procedure.
This distinction matters.
A mature quality system does not measure success by the number of procedures produced.
Instead, the organization should determine which processes require documented information based on factors such as complexity, risk and criticality. ISO guidance explicitly recognizes multiple ways of documenting processes, including written instructions, checklists, flowcharts, visual media and electronic methods.
For a steel plant, this suggests a risk-based approach.
The greater the consequence of variation or incorrect execution, the stronger the justification for formal process control.
Where SOPs Add the Most Value in a Steel Plant
Almost every production area can benefit from some form of standardized work, but documentation should be prioritized according to operational risk and process criticality.
Typical areas include:
Steelmaking
- furnace preparation;
- charging;
- alloy additions;
- tapping;
- ladle preparation;
- temperature control.
Continuous casting
- start-up and shutdown;
- mold preparation;
- tundish practices;
- cooling-system checks;
- abnormal casting conditions.
Rolling and finishing
- mill setup;
- roll changes;
- line threading;
- dimensional control;
- cooling practices;
- inspection and disposition.
Quality control
- sampling;
- specimen preparation;
- dimensional inspection;
- mechanical testing;
- surface classification;
- laboratory practices.
Maintenance
- inspections;
- lubrication;
- equipment isolation;
- component replacement;
- calibration checks.
Material handling and logistics
- coil handling;
- crane operations;
- identification;
- packaging;
- loading;
- traceability.
The goal is not to document everything equally.
It is to control what matters.
How to Build an Effective Steel-Plant SOP
An SOP should begin with the process, not with the document template.
A practical development sequence can follow these steps.
Step 1 — Define the Process and Objective
Clearly establish:
- where the process starts;
- where it ends;
- expected output;
- responsible functions;
- relevant specifications.
Without a clear boundary, procedures tend to become excessively broad.
Step 2 — Identify Critical Risks and Variables
Ask what could affect:
- safety;
- product conformity;
- equipment;
- productivity;
- environment;
- traceability.
This helps distinguish critical controls from administrative detail.
Step 3 — Observe the Actual Work
One of the biggest mistakes in procedure development is writing documents from an office without observing the real operation.
Go to the workplace.
Observe different shifts.
Talk to operators.
Compare the formal process with actual practice.
The gap between work as imagined and work as performed often contains important improvement opportunities.
Step 4 — Define the Standard Method
The procedure should establish the approved sequence and critical controls.
Where multiple methods currently exist, the team should determine whether they represent legitimate operational alternatives or unnecessary variation.
Step 5 — Define Acceptance and Escalation Criteria
Operators need to know not only what normal operation looks like but also what to do when conditions leave the expected range.
A good SOP should answer:
What is acceptable?
What requires adjustment?
What requires escalation?
What requires stopping the operation?
Step 6 — Validate with the People Who Perform the Work
Operators, maintenance professionals, process engineers, quality specialists and safety personnel should participate where relevant.
This improves both technical accuracy and practical usability.
Step 7 — Train and Verify Competence
Publishing a document is not implementation.
Affected employees should understand the procedure and demonstrate the necessary competence before independent execution of critical tasks.
Step 8 — Monitor Effectiveness
After implementation, evaluate whether the procedure actually improves the process.
Relevant indicators may include:
- defect rate;
- rework;
- scrap;
- downtime;
- process deviations;
- safety incidents;
- cycle time;
- yield;
- maintenance failures;
- customer complaints.
ISO process guidance similarly emphasizes monitoring and measurement using indicators such as failure rates, waste, costs, incidents, supplier performance and lead times.
Document Control Is as Important as Document Creation
A technically excellent SOP becomes dangerous if operators use an obsolete revision.
Document control therefore needs to ensure that:
- procedures are approved before release;
- revisions are identified;
- current versions are available at the point of use;
- obsolete versions are removed or clearly identified;
- responsibilities for review are defined;
- relevant records remain retrievable.
Document-control principles place particular emphasis on approval, revision status, availability at points of use and preventing unintended use of obsolete documents.
This becomes increasingly important as plants manage hundreds or thousands of controlled documents.
Digital SOPs Are Changing Shop-Floor Documentation
Industrial documentation is moving steadily from static paper toward connected digital systems.
A digital SOP may include:
- photographs;
- diagrams;
- videos;
- interactive checklists;
- QR-code access;
- electronic signatures;
- revision notifications;
- automatic data capture;
- links to maintenance history;
- real-time process information.
ISO 10013:2021 reflects the evolution of documented information toward digitization, appropriate security measures and greater automation in process workflows.
For steel operations, the main benefit is not simply eliminating paper.
It is connecting the right instruction to the right person at the right equipment with the correct revision.
Industrial digital-documentation systems are already designed around this principle, including mobile field access and single-source-of-truth document strategies for steel-plant operations and maintenance.
SOPs, MES and Smart Manufacturing
The next stage is integration between standardized work and operational systems.
Manufacturing Execution Systems (MES), CMMS platforms, sensors and industrial data systems can increasingly provide context to operating instructions.
Imagine a maintenance technician scanning an equipment identification code.
Instead of searching through folders, the system could present:
- current work instruction;
- equipment history;
- required spare parts;
- safety information;
- inspection points;
- previous abnormalities;
- required completion records.
Likewise, production systems can guide operators according to product route, equipment condition or process state.
This evolution is particularly relevant in 2026 because smart manufacturing in the iron and steel industry now has dedicated international guidance. ISO 21763:2026, published in August 2026, covers smart production-process design, smart equipment and smart production, with the objective of supporting productivity and product-quality improvements in iron and steel plants.
The implication is significant:
the future SOP may no longer be a document that operators open. It may become part of the operating system itself.
But Digitalizing a Bad SOP Does Not Make It Better
This is a critical warning.
Companies sometimes digitalize existing documentation without first questioning whether the underlying procedure is effective.
That can simply transform:
bad paper procedure → bad digital procedure.
Before digitalization, organizations should evaluate:
- Is the process correctly defined?
- Is the procedure actually used?
- Are critical parameters clear?
- Are responsibilities defined?
- Are abnormal conditions addressed?
- Is the information still current?
- Does the procedure add operational value?
Technology should improve access, control and execution.
It cannot compensate for poor process engineering.
Common Reasons SOP Systems Fail
Many SOP initiatives fail not because standardization is ineffective, but because the documentation system becomes disconnected from operations.
Common causes include:
- excessive documentation;
- procedures written without operator involvement;
- documents that do not reflect actual equipment;
- ambiguous responsibilities;
- obsolete revisions;
- inaccessible information;
- insufficient training;
- lack of management follow-up;
- procedures written primarily for audits.
One of the worst outcomes is the audit-only SOP: a document that looks excellent during certification but has little relationship with daily work.
An effective SOP should primarily serve the process.
Audit evidence should be a consequence of good operational control, not the sole reason for creating the document.
A Practical SOP Maturity Model for Steel Plants
Steel companies can evaluate their standardization maturity using five levels.
Level 1 — Informal
Processes depend heavily on individual knowledge and verbal instruction.
Different shifts may use different methods.
Level 2 — Documented
Critical activities have procedures, but documentation may still be inconsistent or difficult to maintain.
Level 3 — Controlled
Procedures have defined ownership, revision control, training requirements and systematic availability.
Process deviations are tracked.
Level 4 — Integrated
SOPs connect with quality, maintenance, training, MES or other operational systems.
Performance data is used to improve procedures.
Level 5 — Adaptive
Digital workflows, operational data and analytics increasingly provide context-sensitive guidance while engineering governance controls changes.
The objective is not necessarily to make every activity Level 5.
A simple, stable activity may need only a clear work instruction.
A critical metallurgical process may justify much stronger controls.
Documentation sophistication should follow process risk and complexity.
Frequently Asked Questions
What is an SOP in steel manufacturing?
A Standard Operating Procedure defines the standardized method for executing an activity or process, including responsibilities, critical steps, controls, safety requirements and relevant records.
What is the difference between an SOP and a work instruction?
An SOP generally defines the controlled method and responsibilities for a process or activity. A work instruction normally provides more detailed task-level guidance on how a specific activity should be executed.
Do all steel-plant activities need an SOP?
No. Documentation should be proportional to risk, complexity, process criticality and the need for consistent execution. Over-documentation can make the system less effective.
How often should SOPs be reviewed?
There is no universally appropriate interval for every procedure. Reviews should consider process risk and should also be triggered by changes in equipment, products, regulations, incidents, non-conformities or operating methods.
Can SOPs reduce steel-production costs?
Yes, indirectly and sometimes substantially. Better standardization can reduce unnecessary process variation, rework, scrap, downtime and training errors. However, savings should be measured through operational indicators rather than assumed.
Should SOPs be digital?
Not necessarily. The appropriate format depends on the operation. Digital systems provide advantages in version control, accessibility, multimedia content, traceability and integration, while some environments may still require simple physical instructions.
Are SOPs required by ISO 9001?
ISO 9001 requires organizations to maintain the documented information necessary to support process operation and retain evidence where required, but it does not mean every activity must have a document titled “SOP.” The appropriate level and format of documentation depend on the organization’s processes and risks.
Can AI create industrial SOPs automatically?
AI can assist with structuring documents, comparing revisions, retrieving technical information and identifying inconsistencies. However, critical industrial procedures should remain under qualified human technical review and approval.
AI does not understand the physical process merely because it can generate convincing instructions.
Conclusion: Standardization Should Control the Process, Not Create Bureaucracy
Standard Operating Procedures are sometimes treated as administrative documents required by quality departments.
That interpretation significantly underestimates their potential.
In a well-managed steel plant, standardization connects engineering knowledge, operational experience, safety, quality, maintenance and continuous improvement.
The best SOP is not necessarily the longest.
It is the one that makes the correct operating method clear, accessible, controlled and repeatable.
As steel plants become increasingly digital, procedures will also evolve. Paper documents will coexist with digital work instructions, MES integration, mobile access, real-time data and eventually more intelligent decision-support systems.
But the fundamental principle will remain unchanged:
technology can deliver the instruction, but engineering must define the standard.
For steelmakers pursuing higher productivity, stronger quality and safer operations, the competitive advantage is not simply having procedures.
It is building a system in which the best known method becomes the normal way of working — and every important deviation becomes an opportunity to improve that method.